

All Products
-
Structural Steel Fabrication
-
Heavy Steel Fabrication
-
Metal Steel Fabrication
-
Sheet Metal Fabrications
-
High Rise Steel Building Construction
-
Structural Steel Frame Construction
-
Steel Girder Bridge
-
Steel Truss Bridge
-
Pedestrian Overpass Bridge
-
Prefab Steel Frame
-
Light Steel Framing
-
Galvanized Steel Structure
-
Stainless Steel Fabrication
-
Steel Street Light Pole
-
Overhead Sign Structures
-
Steel Arch Bridges
-
Precast Girder Bridge
-
 Donald McwayneGood team members always offer budget in time and answer questions with patience, great job!
-
 Joseph AlexanderI am feeling fully respected when taking with Grace and she always gave the best advice. The first batch of the bridge panels got are great too. thanks all.
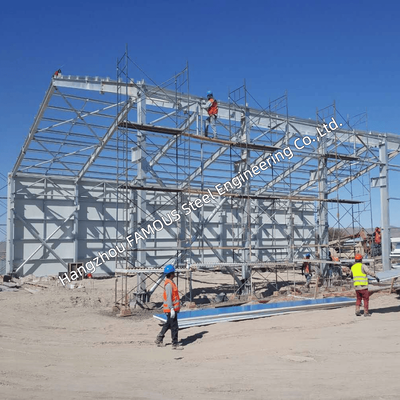
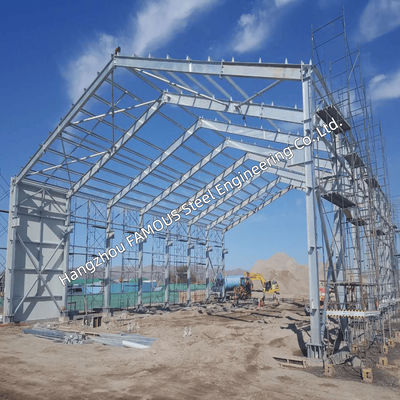
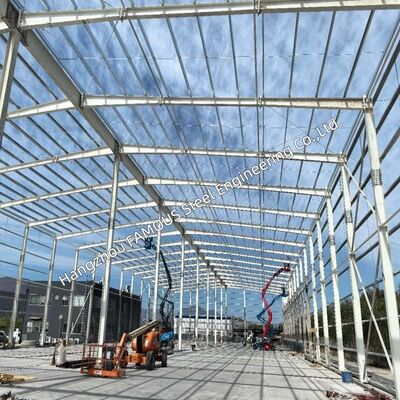
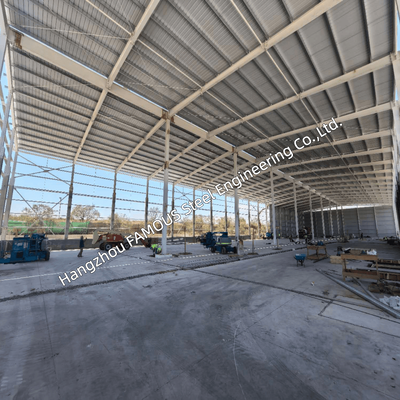
Hot Dip Galvanized Large Steel Shed Warehouse Industrial Steel Buildings Web Truss Rafters UB UC


| Place of Origin | China |
|---|---|
| Brand Name | FASEC |
| Certification | ISO 9001; CE; AS/NZS 1554; AS/NZS 4680 |
| Model Number | Prefab Steel Building |
| Minimum Order Quantity | 1000 MT |
| Price | USD 1,000-1,500/MT |
| Packaging Details | Sea Freight (Container/Bulk Vessel) |
| Delivery Time | 10-30 Days |
| Payment Terms | L/C, D/A, D/P, T/T |
| Supply Ability | 2,000 – 5,000 MT/month |
Product Details
| Product Name | Hot Dip Galvanized Steel Shed & Warehouse Frame | Main Sections | Hot Rolled UC / UB Sections |
|---|---|---|---|
| Roof Rafters | Web Truss Rafters (UB/UC Chords) | Surface Treatment | Hot Dip Galvanized After Full Fabrication |
| Connection | Shop Welded, Site Bolted Splices | Customization | Customized To Customer Requirements (Based On Drawings Or Site Specs) |
Product Description
Galvanizing is not just a coat of paint applied at the end. It is a metallurgical bond formed by dipping a finished steel member into molten zinc. It only works properly if the fabrication sequence and the member details are right before the steel goes into the bath.
Hot Dip Galvanized | Large Steel Shed | Steel Warehouse | Web Truss Rafters | UB UC Columns | Built To Drawing

WHY GALVANIZING IS SPECIFIED
Paint protects steel by sealing it. Once the film is broken by a scratch, cut edge, or site impact, moisture reaches the steel and rust starts underneath—where it cannot be seen. Galvanizing works two ways: the zinc seals the surface, and where that surface is damaged, the zinc beside it corrodes first to protect the steel.
- Barrier Plus Sacrificial: Zinc seals the steel and sacrifices itself at damage points instead of letting the steel corrode.
- Every Surface Coated: Because the member is dipped as a whole, inside faces, cut ends, and hole bores are coated—not just what a spray gun can reach.
- No Site Painting: The frame arrives protected, removing access equipment, weather delays, and second visits from your program.
- Inspectable: Coating mass and thickness can be measured and reported per batch, turning protection into a documented figure.
THE SEQUENCE RULE
One rule governs everything else: All cutting, drilling, welding, and forming must be finished before the member is dipped. A hole drilled after galvanizing exposes bare steel inside the bore, which is exactly where corrosion begins.
- Cut, cope, and notch first so every cut edge receives zinc.
- Drill all bolt, cleat, and fixing holes before dipping.
- Complete all welding (cleats, gussets, stiffeners) before dipping.
- Trial assemble where geometry matters.
- Mark and piece-number using a method that survives the zinc bath.
- Only then clean, flux, and dip.
DETAILING FOR THE BATH
Galvanizing rewards good detailing. These are the details we build into the drawing before fabrication starts:
- Venting: Every closed cavity needs an entry for the zinc and a path for the displaced air.
- Draining: Low points and drainage holes are planned so no pool of zinc solidifies inside a member.
- Distortion Control: Welding sequence, symmetry, and stress relief are planned beforehand for thin plates and long members.
- Threads & Fits: Threaded parts are protected or re-tapped after dipping; bolted faces are detailed to prevent coating buildup.
- Overlapping Surfaces: Surfaces that will never see air are seal-welded so no unprotected gap is left inside.
- Lifting & Handling: Handling points are planned to prevent coating damage between the bath and the site.
GALVANIZING VS. PAINT VS. DUPLEX
| Aspect | Hot Dip Galvanized | Paint System | Duplex (Zinc + Paint) |
|---|---|---|---|
| Protection | Barrier + sacrificial at damage points | Barrier only (damage exposes steel) | Both, with paint slowing zinc consumption |
| Cut Edges & Holes | Fully coated (dipped after fabrication) | Coated only if the painter reaches them | Coated, then over-coated |
| Site Damage | Localized zinc sacrifice, no rust creep | Rust creeps under a broken film | Damage limited by the zinc underneath |
| Maintenance | No routine repainting | Inspection and recoating cycle | Longer cycle than paint alone |
| Appearance | Metallic grey zinc finish | Any color, depends on site conditions | Any color with a zinc base |
| Best For | Industrial sheds, coastal/humid sites | Indoor architectural steel | Projects needing color + max durability |
STANDARDS AND VERIFICATION
Galvanizing is a specification item, not a default. The coating class is chosen against the environment the building sits in: a rural shed, a coastal warehouse, and a fertilizer store should not carry the same specification.
- Galvanizing is carried out to the standard named in your specification.
- Coating class is selected against the site environment and intended service life.
- Coating mass and thickness are measured and reported per batch.
- Adhesion and appearance are checked as part of the batch inspection.
- A report is issued with the delivery documents, alongside mill test certificates.
THE FRAME UNDER THE COATING
The coating protects whatever the frame is. In this package, the frame consists of:
- UC Columns: Rolled universal column sections or welded built-up H sections, with base plates, stiffeners, and knee plates completed before dipping.
- UB Members: Roof beams, tie beams, gable members, and lintels in hot-rolled universal beam sections.
- Web Truss Rafters: Chords in UB or UC with welded vertical/diagonal web members, jig-welded and checked before coating.
- Secondary Steel: Galvanized purlins, girts, bracing, and sag rods, so the secondary frame does not become the first item to corrode.
WHERE GALVANIZING EARNS ITS PLACE
- Coastal and Marine Air: Salt settles on steel and holds moisture; galvanizing reaches cut ends and hole bores where paint fails first.
- Humid and Condensing Buildings: Cold stores, wash-down areas, and process buildings where the frame sees internal moisture.
- Fertilizer, Salt, and Chemical Storage: Aggressive atmospheres where a paint film would be attacked at every defect.
- Exposed and Hard-to-Maintain Frames: Canopies, open sheds, and high frames where repainting means access equipment and a shutdown.
WHAT YOU CAN SPECIFY
- Coating: Galvanizing standard, coating class for your site, duplex with primer/topcoat (including color), and inspection requirements.
- Frame: UC column section, base fixity, knee detail, rafter type (truss or solid UB), truss depth, purlins/girts, and crane runway framing.
- Building: Span, length, bay spacing, eave height, roof pitch, single/multi-span layout, cladding types, and drainage.
- Design Basis: Wind region, roof live load, seismic parameters, and service life expectation (which drives the coating class).
If the building sits near the coast, stores salt/fertilizer, or will be washed down, tell us at the enquiry stage. The frame section may not change, but the galvanizing specification and duplex decision will—and that is much cheaper to settle before fabrication.
PACKAGE AND DOCUMENTS
- Galvanized UC columns with base plates, stiffeners, and knee plates.
- Galvanized UB beams, tie beams, and gable members.
- Galvanized web truss rafters with bolted site splices.
- Galvanized purlins, girts, bracing, sag rods, and fly braces.
- Framed openings, gutter, and canopy brackets.
- Structural bolts, anchor bolts, and fixing accessories.
- 3D model, general arrangement drawings, erection drawings, and anchor setting plan.
- Mill test certificates per heat number, coating report, and packing list.
FROM SPECIFICATION TO DELIVERY
- You confirm the building dimensions, site environment, and coating requirement.
- We detail the frame, set the galvanizing specification, and provide a quote.
- Drawings are issued for approval, with vent and drain details shown.
- Members are cut, drilled, welded, and trial-assembled before any coating.
- The finished frame is hot-dip galvanized, inspected, and issued with a coating report.
- Members are packed with protection and loaded in erection sequence.
Tell us the site and the service life you need. We will confirm the galvanizing specification and whether a duplex coating is the right call for your building.
About Us: Hangzhou FAMOUS Steel Engineering Co., Ltd. is an integrated structural steel manufacturer and global exporter, specializing in custom-engineered steel buildings, bridges, and heavy structures.
🌐 https://www.famoussteel.com/ | https://www.steelfabricat.com/
Recommended Products